Lightweighting is the constraint behind a lot of product design. Whether you are holding a gimbal for hours or flying a drone where every gram buys flight time, you eventually hit the limit of aluminium and ask the obvious question: should this part be magnesium instead?
This comparison stays with the physics and the cost, because the two materials are not interchangeable. We cast both, so the aim here is an honest read, not a sales pitch.
1. The physics: the weight gap
Aluminium density is about 2.7 g per cubic centimetre. Magnesium is about 1.8. That makes magnesium roughly a third lighter at the same geometry, so a one kilogram aluminium housing comes out near 670 grams in magnesium.
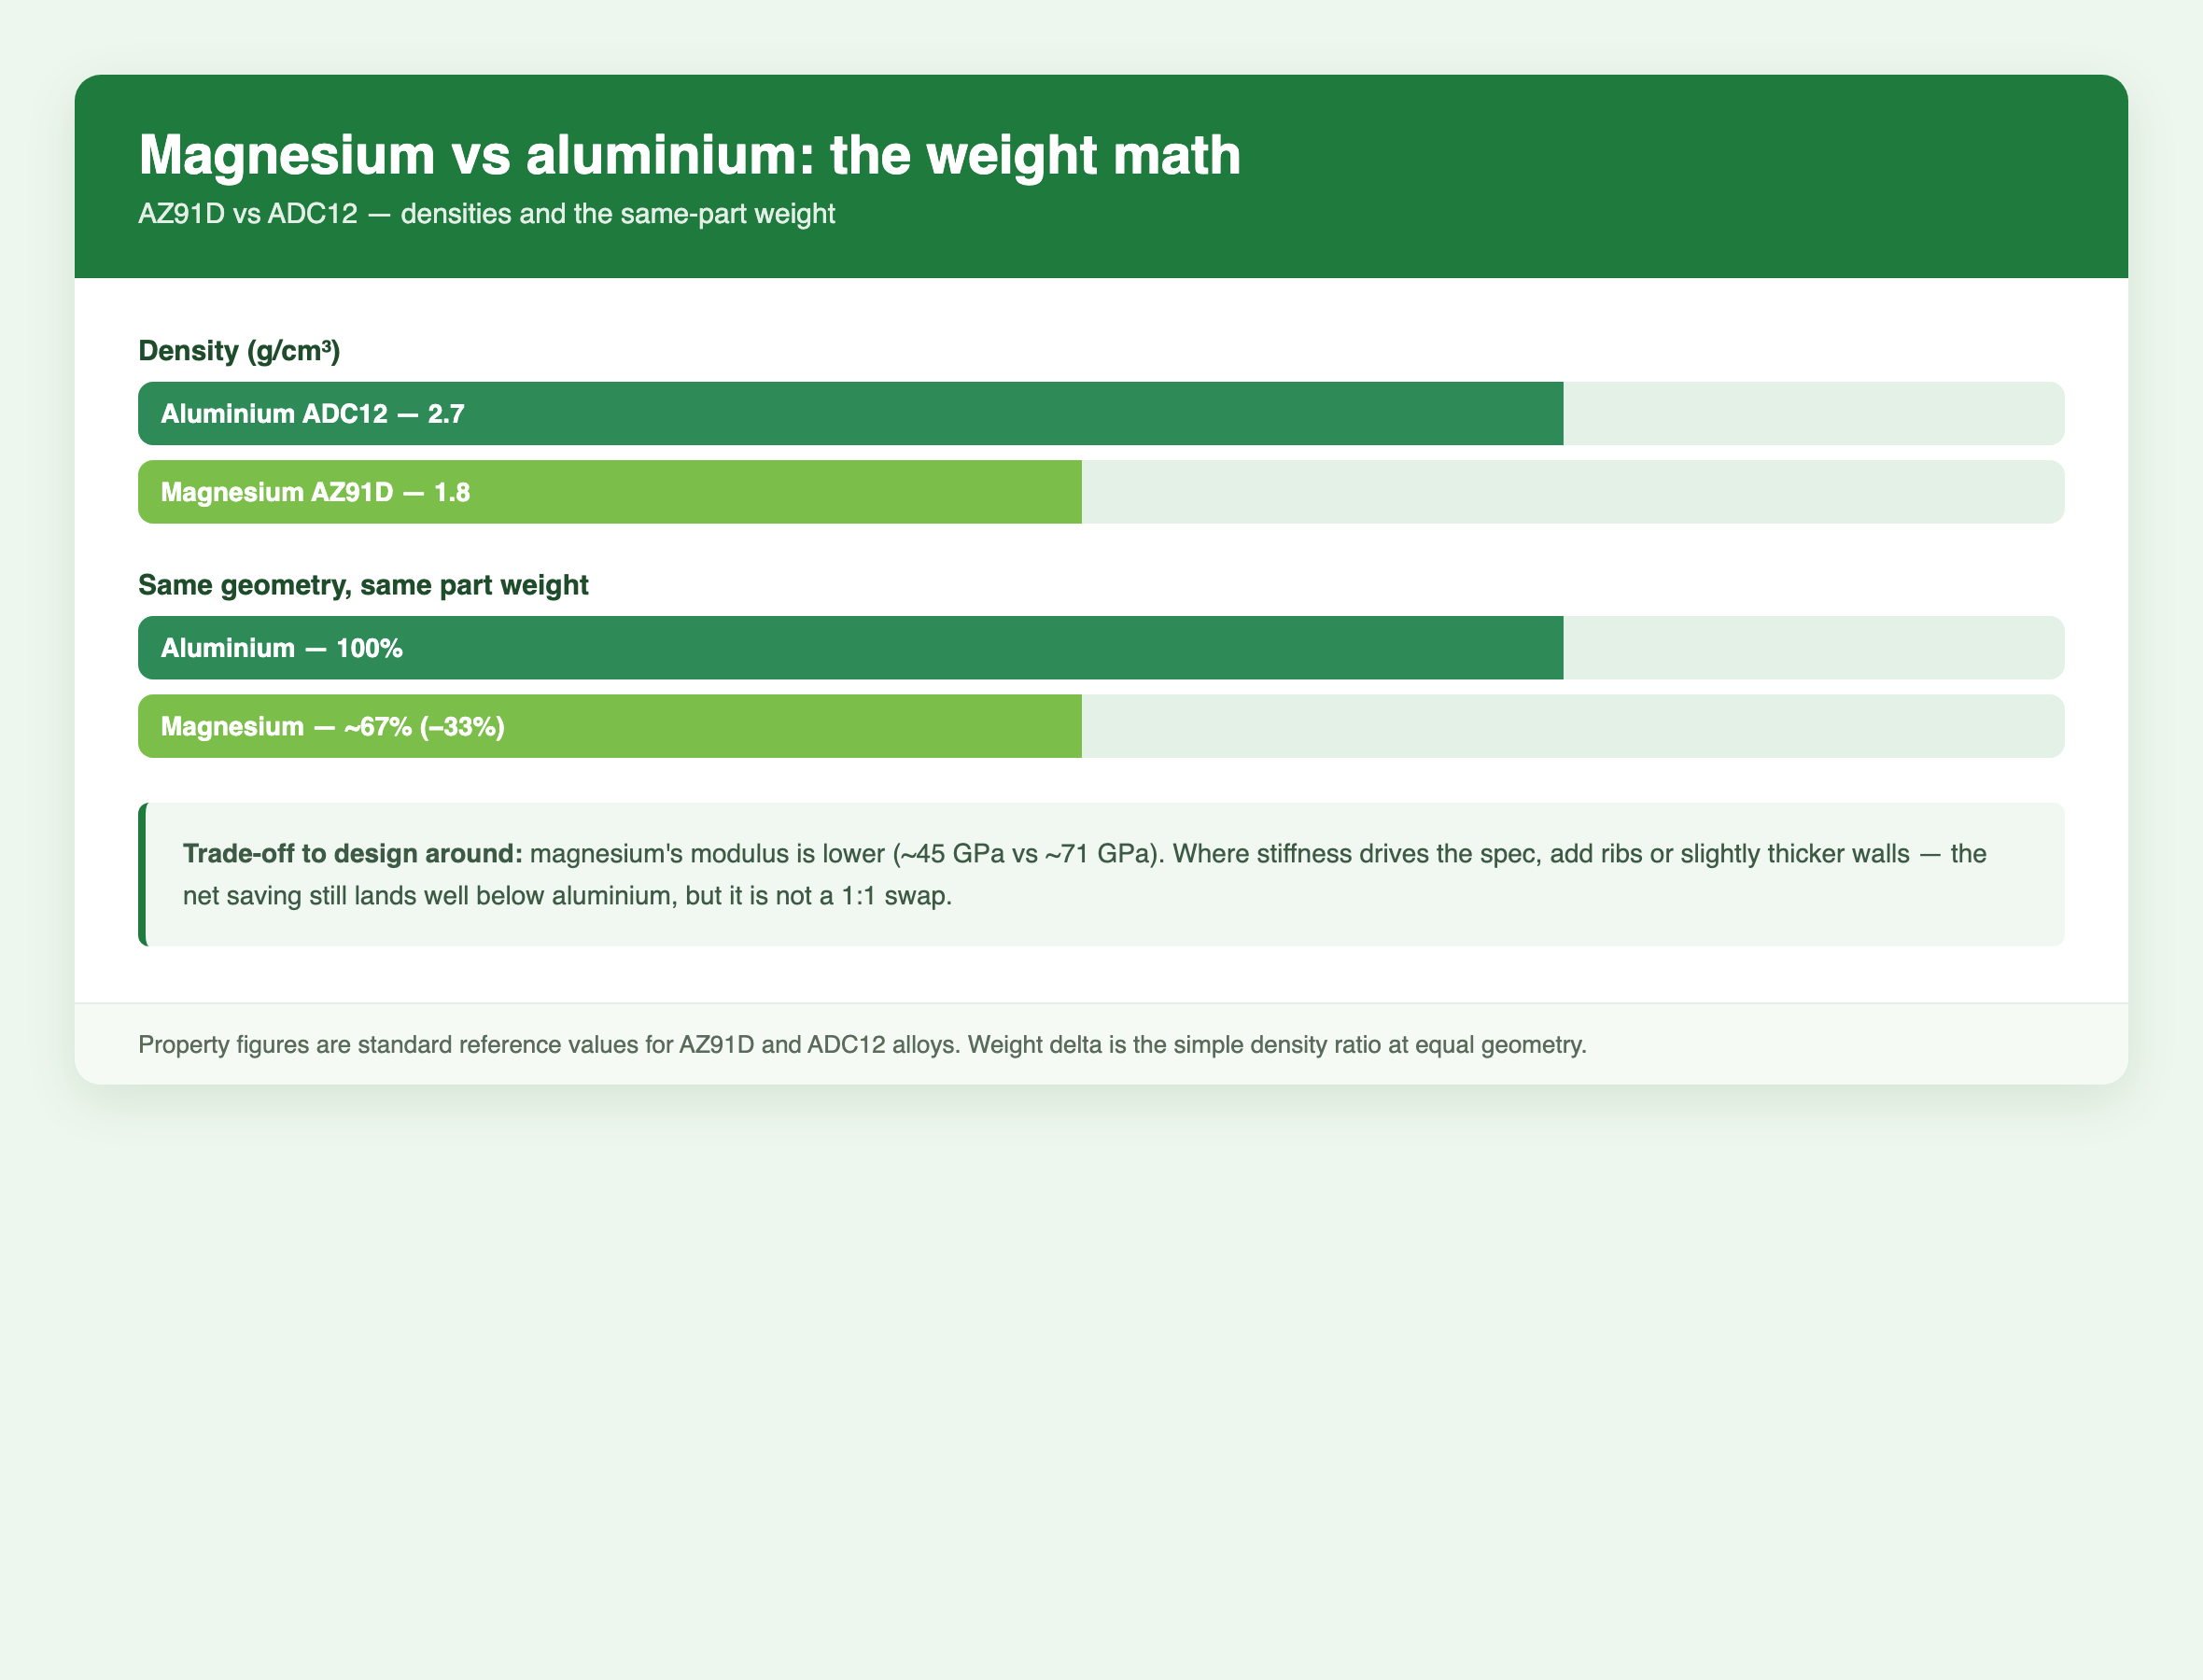
The nuance is stiffness. Magnesium’s modulus sits near 45 GPa against aluminium’s roughly 71 GPa. If stiffness drives the spec, you cannot swap 1:1. You add ribs or thicken walls, and the real saving narrows but still lands well below aluminium. The net benefit has to be calculated per geometry, not assumed.
2. The process: hot chamber versus cold chamber
Aluminium (ADC12) is a cold-chamber alloy. The melt is ladled into the sleeve, high pressure follows, and cycle times are longer because the metal sits in the sleeve. Tool life against aluminium attack on H13 steel is often quoted around 80,000 to 100,000 shots.
Magnesium (AZ91D) is usually a hot-chamber alloy, with the injection mechanism submerged in the bath. That cuts cycle time by roughly 20 to 30 percent and extends tool life toward 200,000 to 300,000 shots, because magnesium is gentler on the steel. Those are general industry reference figures, and the real numbers move with part size and wall thickness.
3. Corrosion and cost reality
Magnesium corrodes more readily than aluminium and needs a disciplined protection sequence, from plating through to coating. That adds process steps and cost. It is also not automatically cheaper: the material premium can outweigh the weight saving unless volume is high enough to recover tooling and the faster cycle.
The honest summary is that magnesium wins when weight is the dominant metric and the part is thin-wall and high volume. Aluminium wins when stiffness, corrosion exposure, and total cost matter more.
4. Magnesium in 2026: humanoid, low-altitude, and semi-solid
New demand is pulling magnesium into places aluminium used to own. Industry observers such as casting-campus list humanoid robot joint housings and drone or eVTOL structural parts among the fast-growing non-automotive casting applications, where thin-wall magnesium saves grams that matter. On the process side, semi-solid and thixomolding routes are being used to fill thin walls and control oxidation in magnesium.
For a mid-size caster this is a market signal worth designing for, not a capability we claim to lead. The parts suit thin-wall aluminium and magnesium work on 88 to 800 tonne machines rather than mega-presses.
5. A decision checklist
Is weight the dominant metric, or is stiffness and corrosion exposure?
What is the annual volume, because tool life and cycle time only pay back at scale?
What corrosion-protection sequence does the part need, and is it validated?
Have you run a stiffness-driven redesign, or just swapped the material?
6. Where Sureton fits
Sureton casts both aluminium and magnesium on 88 to 800 tonne machines, with ISO 9001 in place and IATF 16949 for automotive programs. We will run the stiffness and cost trade-off with you and recommend aluminium, magnesium, or a hybrid rather than pushing one material.
If the part is a robot or cobot component, our cobot arm and gearbox housing guide covers the tolerance story. The tooling cost guide shows when casting beats machining, and the design-for-assembly guide explains part consolidation. For the process basics, start at how die casting works.
Related guides in this topic
Authoritative references
Independent third-party standards and industry bodies, provided for further reading. Sureton is not responsible for third-party content.