
When you review a die casting quotation from Sureton, you may notice a small but important detail. For your zinc parts we quote a hot chamber machine, and for your aluminum parts we quote a cold chamber machine. This is not a matter of preference. The choice is fixed by physics, and it drives your cycle time, your tool life, and your unit cost. This guide explains how hot chamber and cold chamber die casting work, where each one fits, and how the zinc hot chamber process is regaining ground in 2026.
1. The temperature limit: why aluminum cannot use a hot chamber
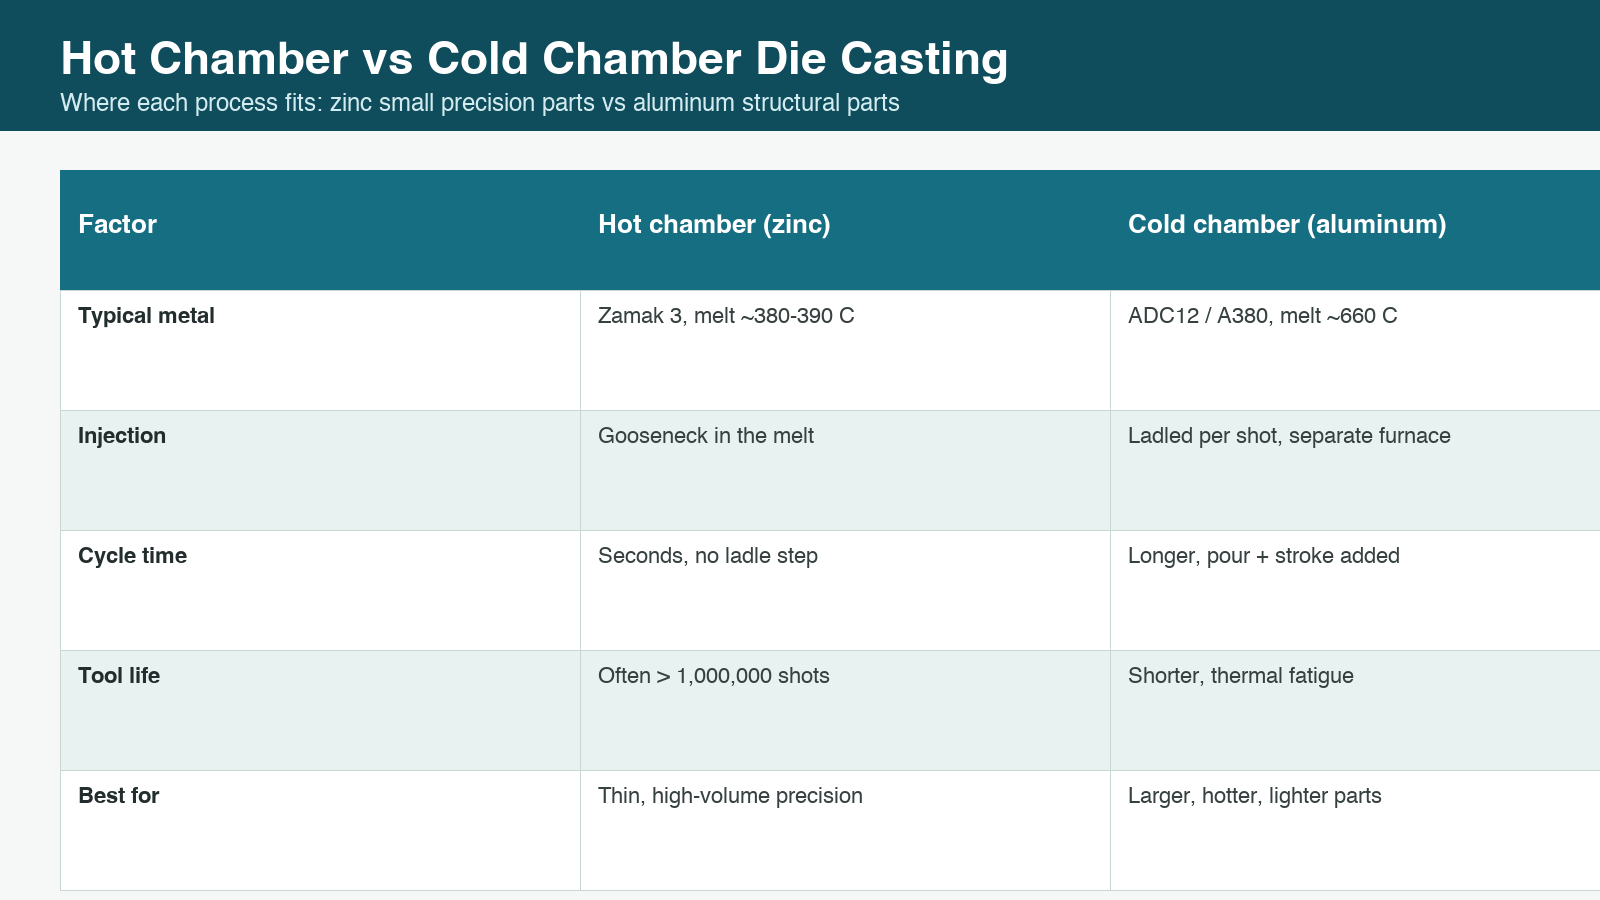
The dividing line is the melting point of the metal and what it does to the injection system. Zinc alloys such as Zamak 3 melt near 380 to 390 degrees C and are poured at roughly 420 degrees C. That is cool enough that the gooseneck, plunger, and nozzle of a hot chamber machine can sit permanently immersed in the molten metal without dissolving.
Aluminum melts near 660 degrees C. At that temperature a steel injection system immersed in the melt would erode within hours. So aluminum is kept molten in a separate furnace and a measured shot is ladled or metered into the cold chamber only at the moment of each cycle. The machine is cold until the shot arrives, which is where the name comes from. The practical consequence is simple: zinc runs hot chamber, aluminum runs cold chamber, and the tooling geometry follows from that fact.
2. The speed factor: hot chamber cycles faster
Because the zinc machine already holds the metal, there is no ladling step. The plunger simply strokes and fills. Typical hot chamber zinc cycles run from a fraction of a second up to a few seconds depending on part size, and high-volume small parts can reach several hundred shots per hour.
Cold chamber aluminum adds the ladle, the pour, the plunger stroke, and a slower fill because the metal cools as it travels. Cycle times are longer, often several times longer than an equivalent zinc shot. For high-volume small components this speed gap is the single biggest reason zinc hot chamber stays competitive even when aluminum is the “obvious” material choice.
3. Tooling economics: zinc dies outlast aluminum dies
Tooling life is where the two processes diverge most sharply. A hot chamber zinc die, running at low melt temperature against a soft alloy, routinely reaches well beyond one million shots before major rebuild. A cold chamber aluminum die fights thermal fatigue, erosion, and solder every cycle, and die life is commonly a fraction of that.
The cost math is not just about the die price. It is about shots per dollar of tooling, and about how often you interrupt production to rebuild. For long runs of small zinc parts, the hot chamber process spreads tooling cost over many more good parts. When you compare a zinc quote against an aluminum quote, look at the amortized tooling, not the headline mold price. Our die casting tooling cost guide walks through that amortization.
4. Zinc hot chamber in 2026: a process regaining ground
Zinc hot chamber die casting is not a legacy process fading out. Third-party market research shows the automotive parts zinc die casting market at roughly USD 5.1 billion in 2025, projected near USD 5.3 billion in 2026, with pressure die casting holding about 71 percent of that volume in 2025 specifically on the strength of hot chamber productivity. The same research points to net-shape zinc components cast in hot chamber machines displacing machined steel brackets, multi-piece stamped assemblies, and polished aluminum housings as electrification and Euro 7 compliance push automakers toward thin-walled, tightly toleranced castings.
These figures are market research and OEM sector observations, not Sureton production data. We cite them to show the direction of the industry, not to claim a share of it. For buyers the takeaway is durable: specify zinc hot chamber where small, thin, high-volume precision parts are involved, and you benefit from faster cycles and longer tool life than an aluminum route would allow.
5. Pressure and density: what each process can hold
Hot chamber zinc runs at lower injection pressure than cold chamber aluminum, which is acceptable because zinc fills thin sections readily at lower pressure. Cold chamber aluminum needs higher pressure to fill and to suppress porosity in thicker sections. Both can deliver sound parts; they just operate in different pressure and section-thickness envelopes.
If your part needs pressure tightness or low porosity for a sealed function, the process choice interacts with your alloy and your wall thickness. Our precision zinc small parts guide covers how thin sections and tight tolerances are held on zinc, and our zinc versus aluminum comparison helps you weigh the two materials before you commit tooling.
6. Making the choice: it is about total cost, not the machine
The right question is not “which machine is better” but “which process gives the lowest total cost for this part over its lifetime.” Answer it with four inputs: annual volume, target wall thickness, required tolerances, and post-machining burden. High volume with thin walls and light tolerances favors zinc hot chamber. Larger structural sections, higher operating temperature, or a need for aluminum’s lower density favors cold chamber aluminum.
When the material is genuinely open, run both quotes through tooling amortization and scrap assumptions rather than comparing piece price alone. The ADC12 versus A380 alloy selection guide and the tooling cost guide above give you the numbers to do that honestly.
Summary: match the process to the part
Hot chamber zinc and cold chamber aluminum are not interchangeable, and they are not in a race. Zinc hot chamber wins on speed and tool life for small, thin, high-volume precision parts, while cold chamber aluminum covers larger, hotter, lighter structural work. In 2026 the zinc hot chamber process is gaining share precisely because electrification rewards the parts it does best. Send us your drawing and we will tell you which route your part actually belongs in.
Related guides in this topic
Authoritative references
Independent third-party standards and industry bodies, provided for further reading. Sureton is not responsible for third-party content.


