
A die casting tool is the single largest fixed cost in a program, and the one buyers ask about least. Tooling price, amortization, and break-even volume decide whether die casting beats machining or molding, and they decide how a program survives a demand swing. This guide breaks the tooling cost down the way a quoting engineer actually sees it, so you can read a quote and know what you are paying for.
1. What the tooling price actually includes
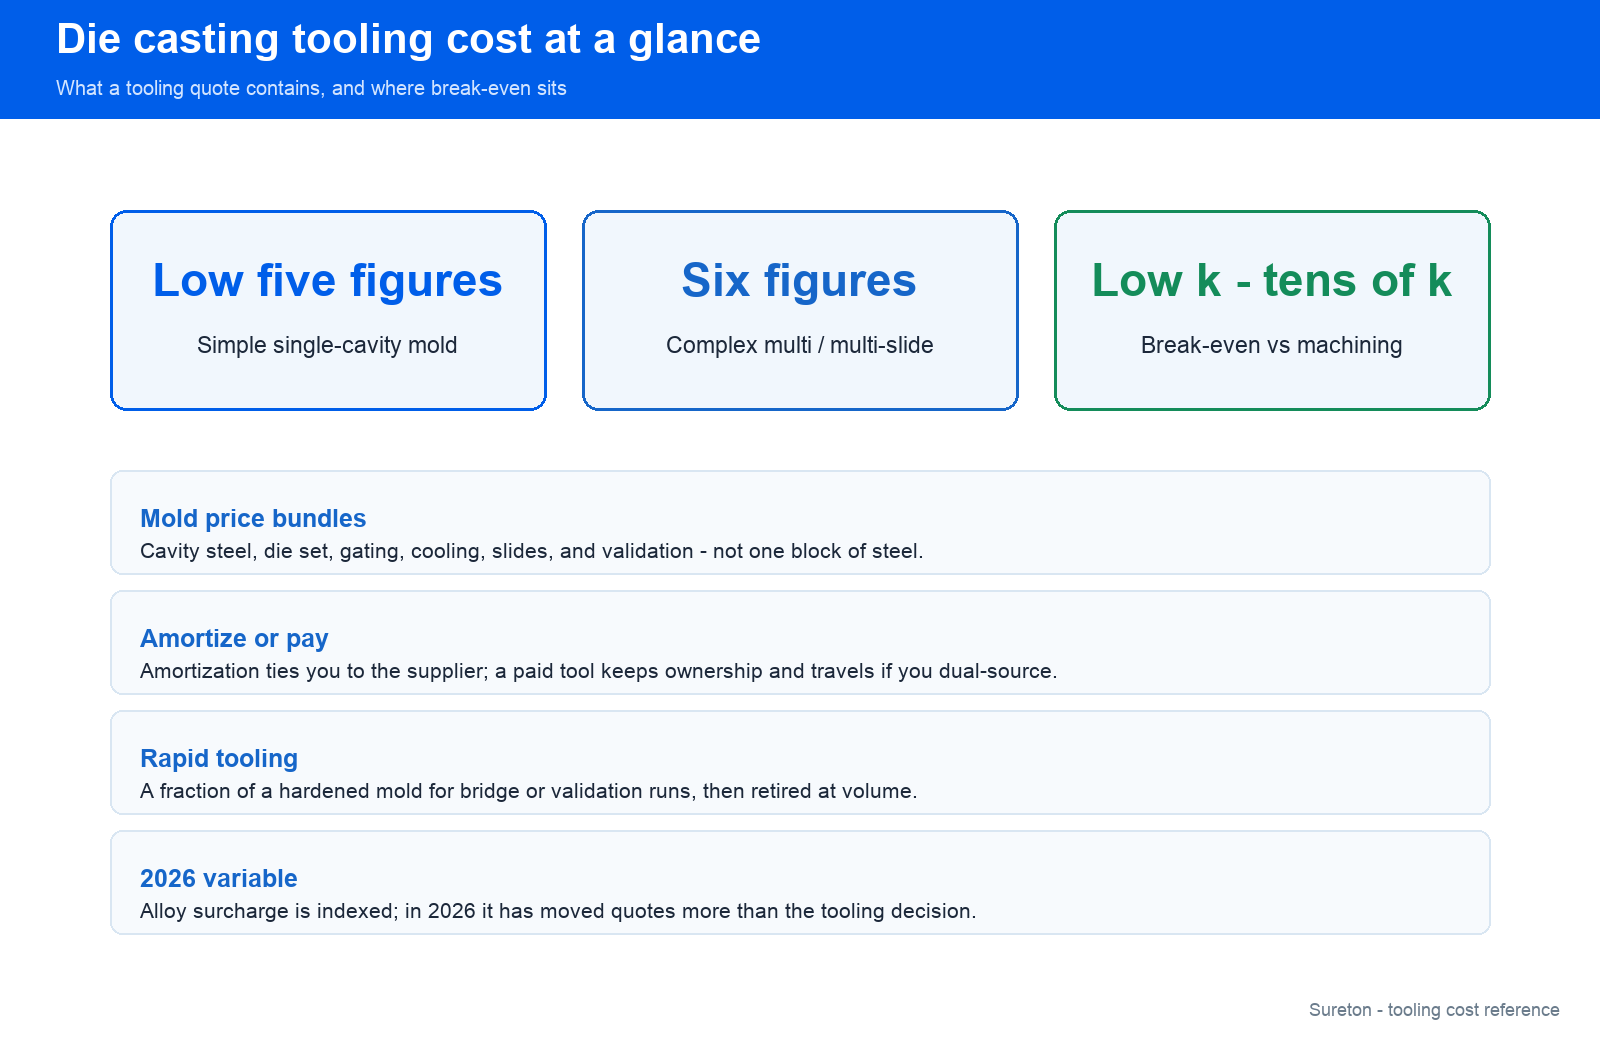
A die casting mold is not one block of steel. The quote bundles the cavity and core steel, the die set, the runner and gating, cooling and ejection, any slides or cores for undercuts, and the machining and validation time to get it shooting good parts. A simple single-cavity tool for a small part can land in the low five figures, while a multi-cavity or multi-slide tool for a complex housing runs well into six figures. The number moves with part size, cavitation, and how many moving elements the geometry demands. Treating the mold price as a single line is the first mistake buyers make.
2. Amortization versus a hard tooling charge
Most programs spread the mold cost across the parts instead of billing it up front. Amortization lowers the per-part price once volume justifies it, but it ties you to the supplier for the agreed quantity. A hard tooling charge, paid once, keeps the unit price flat and the tooling ownership clear. Neither is universally better: amortization helps cash flow at low volume, while a paid tool travels with you if you ever dual-source. The right structure follows your volume and your sourcing strategy, and a good quotation states which one you are being offered.
3. Where the break-even with CNC sits
Die casting wins on unit cost at volume because the mold cost is spread thin, but it loses on setup cost at low volume because the tool still has to be built. A common rule of thumb puts the cross-over with machining somewhere in the low thousands to tens of thousands of parts, depending on geometry. Below that, CNC or a rapid tooling route is often cheaper once you count the mold. Above it, die casting pulls ahead on material yield and cycle time. Our low-volume and rapid tooling guide covers the bridge range where the decision is closest.
4. Rapid tooling and the bridge volume
Rapid or soft tooling uses a lower-cost steel or a bridge process to get parts made before committing to a production hard tool. It typically costs a fraction of a hardened mold and suits bridge production or design validation, then it is retired when volume justifies the real tool. The trade-off is life: a rapid tool may be rated for tens of thousands of shots rather than the hundreds of thousands a hardened tool reaches. For programs under roughly a few hundred parts a year, machining or a rapid tool often beats building a production mold at all.
5. A 2026 cost variable: alloy surcharge indexation
The mold is fixed, but the metal is not. Aluminum and zinc alloy prices move with commodity markets, and many suppliers index the material surcharge to a published rate rather than quoting a flat number. In 2026 that indexation has been the swing factor in year-over-year quotes, sometimes moving the part price more than the tooling decision does. Read the surcharge clause before you compare quotes, because two tools at the same mold price can carry very different material exposure. This is an industry observation on cost structure, not a Sureton price list.
6. Design choices that change the tooling bill
The geometry decides the tool cost more than the material does. Generous draft, uniform wall thickness, and features that avoid slides or side cores keep the mold simple and the price down. Part consolidation, where one casting replaces several stamped or machined pieces, can justify a more complex tool because it removes downstream operations. Our design-for-assembly guide shows how to spot those consolidations early, before the steel is cut.
The takeaway
Tooling cost is a structure, not a number. Read the mold price as steel plus movement plus validation, decide amortization against your volume, and check the alloy surcharge clause before you compare programs. Send the drawing with your expected annual volume and we will tell you whether die casting, rapid tooling, or machining is the honest break-even for this part.
Related guides in this topic
Authoritative references
Independent third-party standards and industry bodies, provided for further reading. Sureton is not responsible for third-party content.


