
1. The geometry reality: concentricity is king
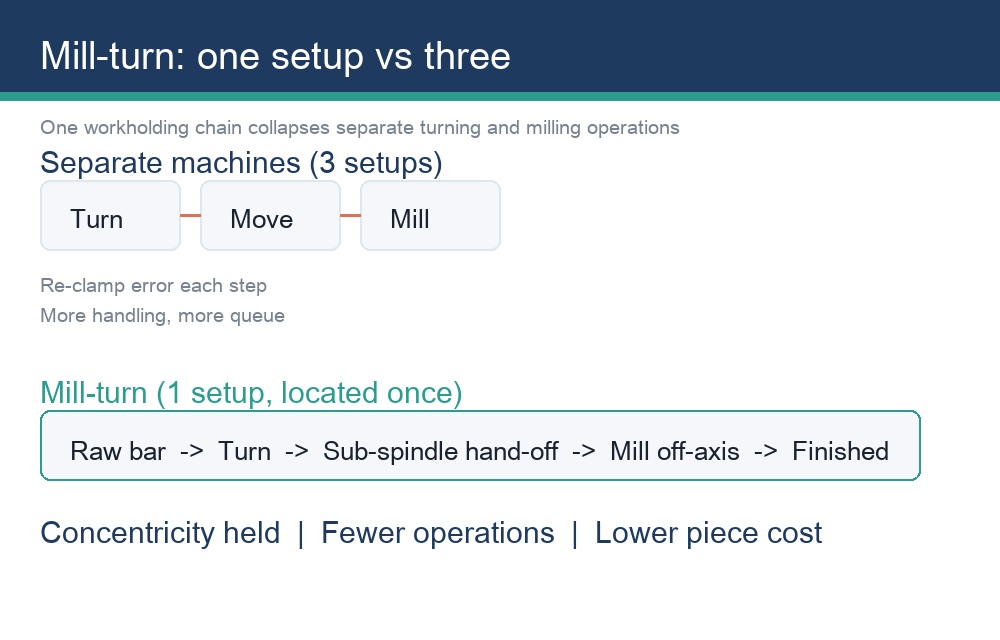
Most precision parts are not pure turned shafts and not pure milled blocks. They are round at the core with features cut off-axis: a flange, a hex, a drilled hole that does not line up with the spindle, a keyway. The classic shop route is to turn the part, unchuck it, walk it to a machining center, re-clamp it, and hope the two setups agree. They often do not.
Every time a part is re-chucked, you reintroduce a locating error between the turned and milled features. For a part that needs its threaded bore to sit concentric with its turned OD, those setups are working against you. Five-axis machining solves similar problems a different way; mill-turn solves this one by never letting go of the part.
2. The sub-spindle hand-off
A mill-turn lathe carries live tooling and usually a second spindle. The main spindle turns and mills one end, then passes the part to the sub-spindle, which holds it by the finished feature while the other end is machined. The part is located once and stays located. The off-axis holes, flats and threads are cut with the part still chucked and spinning under program control.
This is why mill-turn parts hold concentricity that would be a fight across two machines. The geometry that matters is cut in a single workholding chain.
3. The economics: a higher rate, but fewer operations
The machine hour on a mill-turn cell costs more than a standalone lathe. What you buy back is operations. One setup instead of three means no second fixture, no handling between machines, no queue time, and no re-clamping variance. For a part with moderate complexity, the total cost per piece usually drops once you add up the steps you eliminated.
The break-even point is not fixed. It moves with how many separate operations the part would otherwise need and how many you can collapse into one cycle. Parts that are mostly rotational with a handful of milled features sit squarely in mill-turn’s sweet spot.
4. When should you ask for mill-turn?
Rotational core with off-axis features: flanges, hexes, cross-holes, keyways on a turned body.
Concentricity matters: a threaded bore that must stay true to the OD, or a sealed face that must run straight.
Volume justifies the cell: enough repeat quantity that collapsing setups pays back the cycle.
When the part is a flat plate or a pure prism, mill-turn adds little. That is the territory of three-axis versus five-axis trade studies instead.
5. The done-in-one trend in 2026
What changed recently is not the machine concept but the cell around it. Robotic loading and pallet pools now let a mill-turn run long unattended batches, which trims the labor share that used to blunt the economics. Industry reports point to near-lights-out running on high-mix work. Treat that as a supplier-capability question, not a promise: ask a shop whether its mill-turn cells are actually automated before you count on the labor saving.
Ask the right question on the RFQ
Send the drawing and note which dimensions must stay concentric. If mill-turn collapses three setups into one, the part gets cheaper and more consistent at the same time.
Related guides in this topic
Authoritative references
Independent third-party standards and industry bodies, provided for further reading. Sureton is not responsible for third-party content.


