
1. The reality of cast-in threads
It is a conversation we have almost every week at Sureton. A client sends a drawing for a new aluminium housing with a dozen M4 mounting holes and asks whether we can cast the threads directly to remove the secondary machining cost. The short answer is: yes, we can, but you probably do not want to. The idea of a finished part straight from the die sounds like the ideal of cost reduction, yet the physics and the tolerance stack usually make cast-in threads a false economy. Here is the honest breakdown of when to cast, when to machine, and where the break-even point sits.
2. External threads: the flash problem
To cast a bolt-like feature, the die must split to release it, and the parting line runs across the thread. Even with a precise die you get a hairline of flash across the thread path. When the assembly line tries to run a nut onto it, it jams, and you end up chasing the thread with a die anyway. Cast external threads are only viable for very coarse threads, such as a garden-hose connector, where the fit is loose.
3. Internal threads: the unscrewing problem
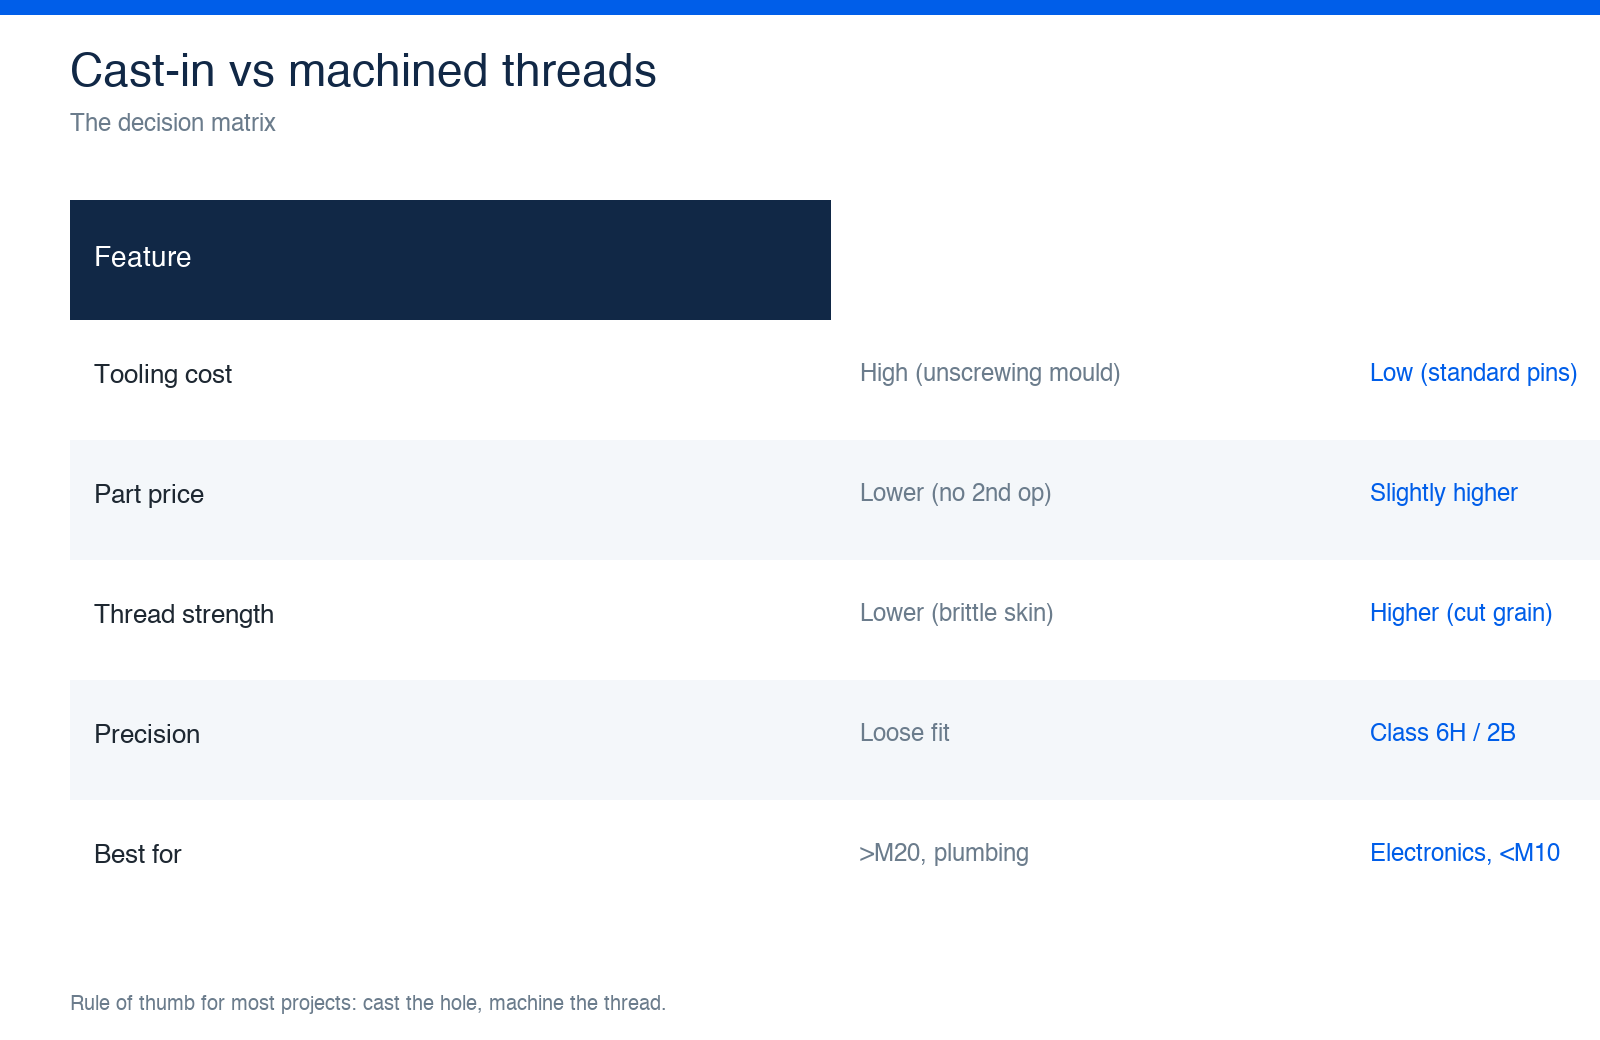
To cast an internal thread the core pin cannot simply pull out, or it would rip the thread. It must unscrew itself before the die opens. That needs a complex unscrewing mould with gears and hydraulic motors, which adds roughly 3,000 to 5,000 dollars to tooling and 5 to 10 seconds per cycle to the casting time. You save machining but pay it back in the mould and the cycle.
4. The M6 threshold we use
Below M6, machine it. The die casting grain is too coarse to hold a fine pitch, and a cast small thread strips if an operator uses a powered driver. We cast the cored pilot hole to minor diameter and then tap it, giving cut threads at Class 6H. Above M6 the thread gets stronger; a large M20 drain plug on an oil pan is a reasonable candidate to cast, because machining a hole that big removes a lot of material slowly.
5. The sweet spot: auto-tapping
Many buyers fear machining because they picture a person with a hand drill beside the press. That is the old way. At Sureton we use multi-spindle auto-tapping centres: the part loads into a fixture and the machine taps a dozen holes at once in seconds, at pennies per part, with machined precision and automated consistency. For high-volume consumer electronics in zinc, self-tapping screws into a smooth cored pilot are often the cleanest route, removing the tapping cost entirely. For the tooling maths behind these choices, see our die casting tooling cost guide.
6. Tolerance: the deal breaker
Die casting typically holds ISO 8062 CT6, meaning a cast feature can move about 0.1 mm with shrinkage. A machine screw needs tight engagement, and a cast thread that shrinks a little more than predicted will not accept the screw. You cannot adjust a cast thread without re-cutting steel; a machined thread is always correct because the tap does not shrink. Our surface roughness and tolerance notes cover how we hold geometry on machined features. The practical rule of thumb holds for the large majority of projects: cast the hole, machine the thread.
7. Optimise your assembly
Do not let a stripped thread stop your line. The best approach is usually to cast the hole and machine the thread. Send us the drawing and our DFM engineers will flag every hole and tell you which to core, which to drill, and which to tap, saving cost without giving up quality. This pairs naturally with insert die casting for local reinforcement, and with the fundamentals in our die casting overview.
Related guides in this topic
Authoritative references
- ASME Y14.5 — Dimensioning and Tolerancing (GD&T)
- NADCA — Product Design for Die Casting (design manual)
Independent third-party standards and industry bodies, provided for further reading. Sureton is not responsible for third-party content.


