
Weight is the defining constraint in electric vehicle engineering. Every kilogram added to the body structure forces a larger battery pack to hold the same range, which adds more weight in a loop that ends only when parts get lighter. Structural aluminum die casting answers that loop by consolidating many stamped and welded steel pieces into fewer aluminum castings.
This article covers where structural casting helps, what changed in the alloys and processes behind it, and how the work splits between very large integrated castings and the smaller structural parts that most supply chains actually buy. We also note where our own 88-800 tonne machines fit, and where they do not.
1. Why EV lightweighting starts with the body structure
In a combustion car, mass is a comfort and efficiency issue. In an EV, it is a range issue. The body-in-white and chassis carry the heaviest fixed load, so a reduction there pays back across the whole pack. Replacing stamped steel assemblies with aluminum castings cuts both part count and joining operations.
Mass: Aluminum at roughly 2.7 g/cm3 is about one-third the density of steel, so a like-for-like component is far lighter before any consolidation.
Stiffness: Fewer joints mean fewer stress concentrations, which helps torsional rigidity and crash load paths.
Assembly: One casting replaces dozens of stampings and hundreds of welds, removing fixture and tolerance-stack work.
2. Part consolidation: from many stampings to fewer castings
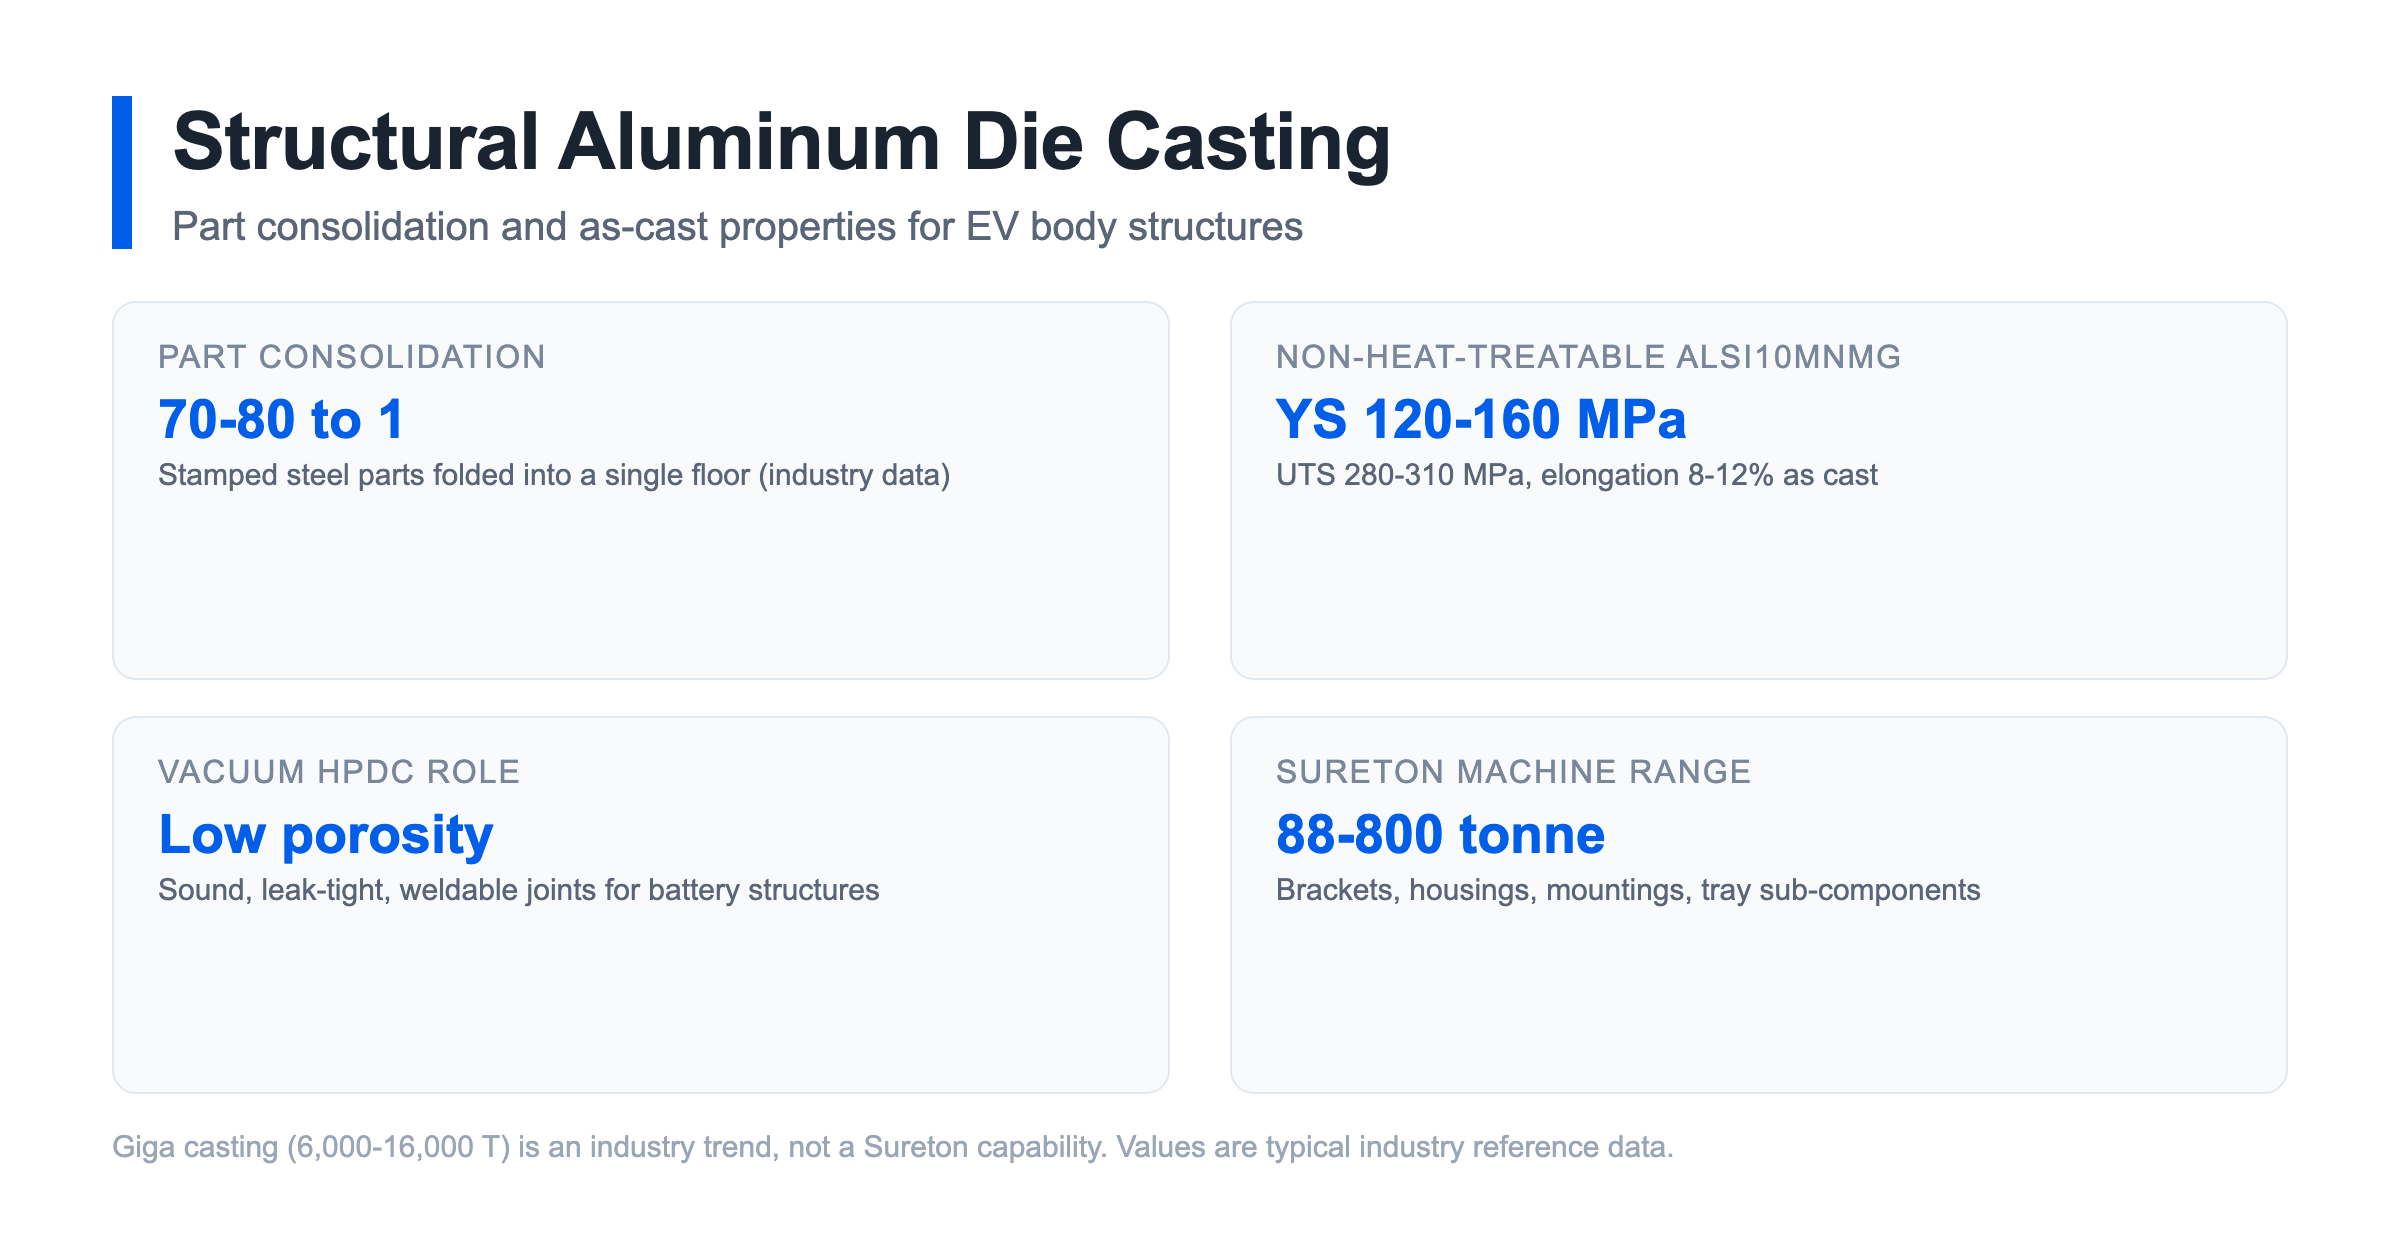
The core idea behind high-pressure die casting for structural use is consolidation. An underbody that was 70 or more separate steel parts becomes one or a few aluminum castings. Industry write-ups of giga casting programs report folding 70-80 stampings into a single floor, and some rear-floor programs cite 70-170 fewer parts and over 1,000 fewer weld joints.
Consolidation is where the cost and mass case is won or lost. It is also where design-for-casting discipline matters most, because a part that cannot be cast cleanly negates every saving.
3. The metallurgy shift: non-heat-treatable aluminum alloys
Standard die-cast grades such as ADC12 or A380 are strong in rigid housings but brittle in a crash, with elongation often below 3 percent. Structural parts need to bend and absorb energy, which pushes toward heat-treatable grades until you hit the real problem: heat treating a large thin-walled casting distorts and blisters it.
The 2026 answer in the industry is non-heat-treatable aluminum alloys formulated for structural HPDC, commonly in the AlSi10MnMg family. Reported as-cast properties run around 120-160 MPa yield, 280-310 MPa tensile, and 8-12 percent elongation, enough for body structural use without a T6/T7 step. These figures are material-supplier and OEM public data, not a Sureton specification, and the exact grade your program needs should be set by your engineering team.
For context on how material choice interacts with part function, see our note on aluminum versus zinc for total cost of ownership.
4. Vacuum HPDC and porosity control
Structural castings must stay tight and sound. Entrained gas porosity is the enemy, because it weakens the section and blocks leak-tight and weldable joints. High-vacuum die casting evacuates the cavity before fill, which is why vacuum assist shows up on structural and battery-related programs.
Porosity is controlled by alloy, gate design, venting, and vacuum level together. Our porosity reduction guide covers the process levers we use on production parts.
5. Giga casting and integrated die casting in 2026
Giga casting, also called megacasting or integrated die casting, refers to very large single-piece structural castings made on presses in the 6,000-16,000 tonne range. Market trackers put the global giga-casting market near USD 3.6 billion in 2026 and growing in the mid-teens percent annually. North American and European automakers have moved several structural parts, rear underbodies, front structures, and battery enclosures, to single-piece castings, with Tesla’s gigapress approach widely cited as the reference design.
This is an industry trend, not a capability we claim. Our machines run 88-800 tonnes, which covers sub-frame brackets, housings, mounting and enclosure structures, and battery-tray sub-components, but not full-size underbody megacastings. We state the boundary plainly so buyers scope programs correctly.
6. Where a mid-tonnage supplier fits
Most EV programs are not one megacasting on a 9,000-tonne press. They are hundreds of smaller structural and semi-structural aluminum parts: battery tray members, brackets, busbar and sensor housings, mountings, and enclosure structures. These are squarely in the 88-800 tonne range and benefit from the same consolidation logic at a smaller scale.
For programs that also need machining and surface finishing, our hybrid die-casting-plus-CNC workflow carries a part from casting through critical-feature machining in one managed process.
7. Design checklist for structural castings
Set the alloy with your team: Decide between a standard grade and a non-heat-treatable structural grade before tooling, since it changes wall and rib design.
Plan for vacuum: If the part must be leak-tight or weldable, specify vacuum assist and design vents and gates for it from the start.
Mind wall and rib rules: Thin-wall sections fill only with the right gate velocity and thermal balance; review thin-wall design limits early.
Budget tooling realistically: Structural tools cost more and run longer; our tooling cost guide helps size the program.
Get a structural casting review
Bring drawings and the target alloy, and we will return a feasibility and process recommendation for your part on our 88-800 tonne line. Share your files for a DFM review.
Further reading on this topic: EV battery tray die casting · lithium battery structural components.
Browse all guides in this topic
Authoritative references
- SAE: giga-casting and lightweight structural strategy
- SAE technical paper: lightweighting cost vs. EV range benefit
Independent third-party standards and industry bodies, provided for further reading. Sureton is not responsible for third-party content.


