
An outdoor die cast part lives or dies by its corrosion protection. The casting can be dimensionally perfect and still fail in the field if the finish breaks down where salt, humidity and temperature swing meet the metal. Salt spray testing is the standard way buyers check that protection before a part ever ships.
This guide explains what salt spray testing measures, how we qualify outdoor aluminium and zinc die castings for 5-year (Standard) and 10-year (Premium) outdoor and UV service, and how to write the requirement so you actually get the protection you paid for.
1. What salt spray testing actually measures
The most widely used method is neutral salt spray under ASTM B117 and its international equivalent ISO 9227. A sample sits in a sealed chamber at about 35 degrees Celsius while a 5 percent sodium chloride solution is sprayed as a fine mist. The part is inspected at set intervals for corrosion.
Two outcomes matter, and they are not the same:
White rust is corrosion of the coating or the zinc layer itself. On a passivated or plated zinc part it is the first thing to appear, and many buyers now treat any white rust within the rated hours as a fail.
Red rust means the base steel or aluminium substrate has been reached. That is a protection failure, not just a cosmetic one.
The rating follows standards such as ISO 10289 or GB/T 6461, where a higher protection rating means less area affected. The test tells you how the coating resists the chamber, not how many years the part survives outdoors, a point worth keeping in mind when someone quotes a salt spray number as a service life.
2. Our salt spray qualification: 480 h (Standard) and 720 h (Premium)
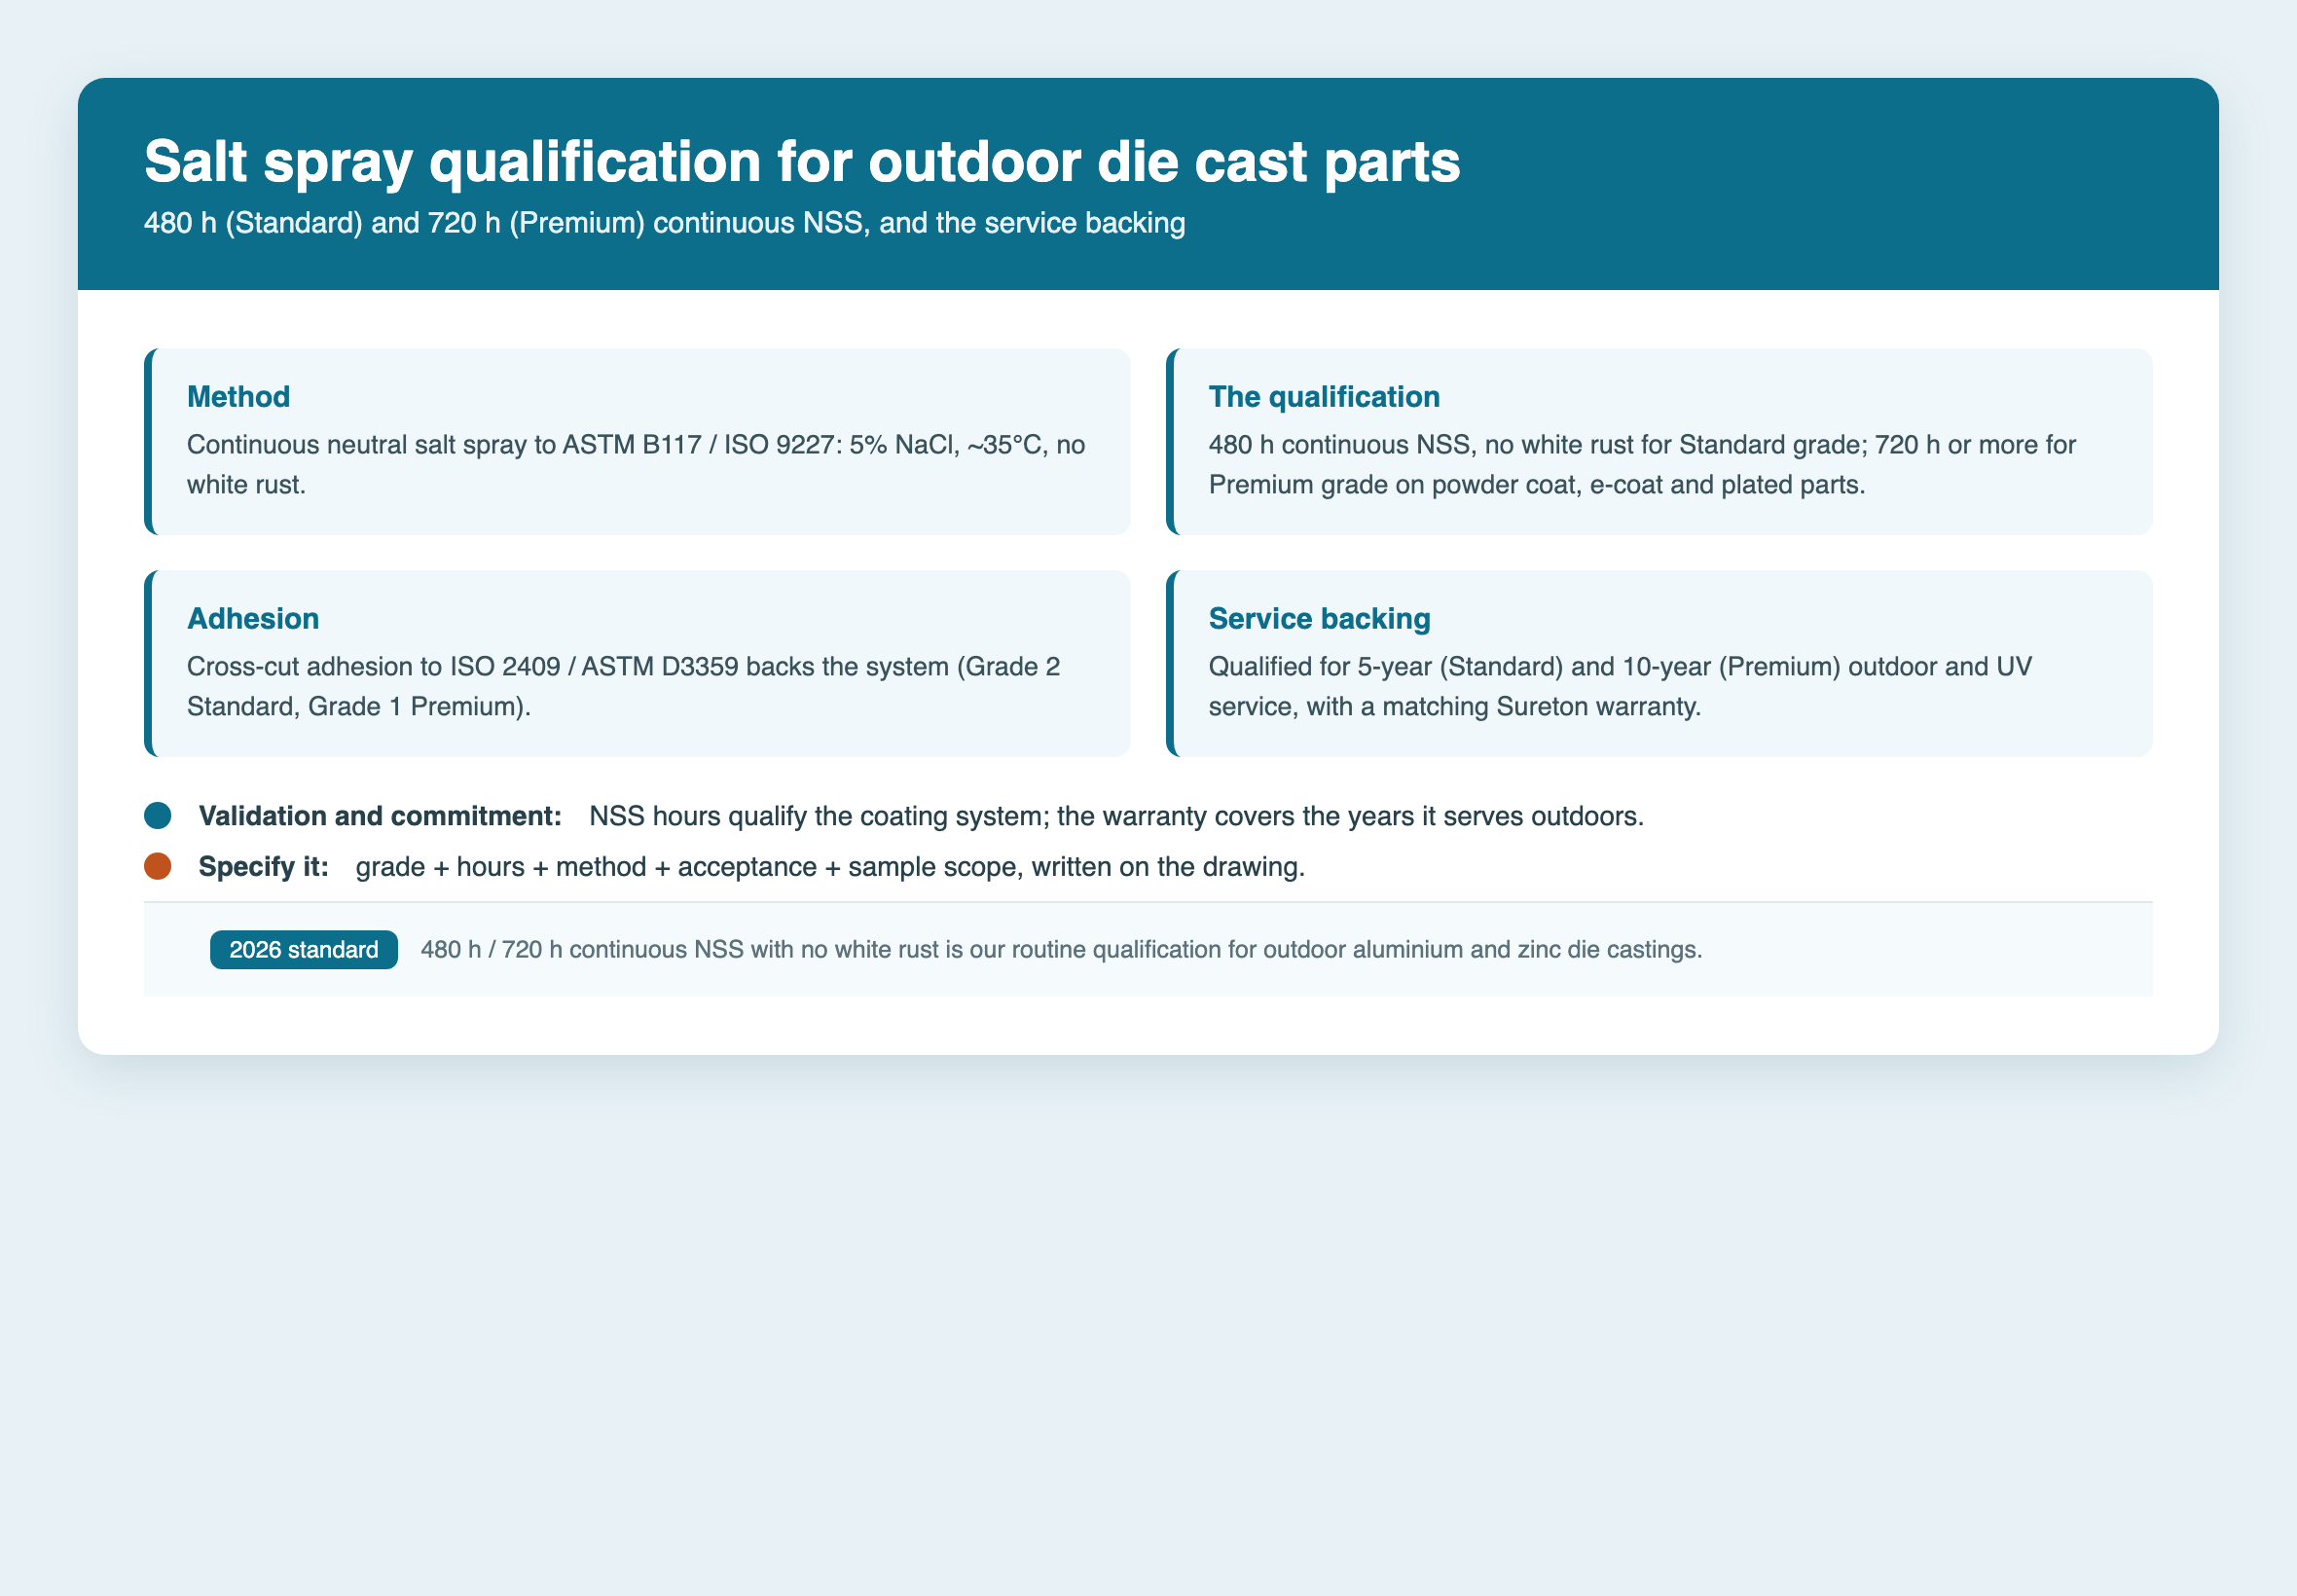
For outdoor die cast components with powder coat, electrocoat or plating, our routine qualification is continuous neutral salt spray (NSS) to ASTM B117 / ISO 9227 with no white rust. Standard grade is qualified at 480 h; Premium grade is qualified at 720 h or more. These thresholds are a gate we run on every exposed batch: they catch poor pretreatment, thin coating and porous substrate quickly, before a batch reaches the field.
The qualification is built on trivalent-chromate passivation plus a sealed powder or e-coat system, and the result is backed by cross-cut adhesion testing to ISO 2409 / ASTM D3359. The hours are the screen; the service qualification they support is what travels with the part. We run this as a standard check on powder coated, electrocoated and plated die cast parts so a corrosion failure shows up in the lab, not at goods receipt.
3. Why the coating choice decides the result
Salt spray performance is mostly a function of the finish, not the casting underneath. The same aluminium or zinc substrate can pass or fail by a wide margin depending on pretreatment and coating.
Powder coating gives a thick, continuous film and is the default for outdoor structural and enclosure parts.
Electrocoating (e-coat) reaches recesses and internal surfaces that spray cannot, which is why it is common under a topcoat.
Plating and anodizing serve decorative and specific functional needs, with their own salt spray expectations.
The choice is a trade between cost, appearance, chemical resistance and the salt spray target. Our comparison of die casting surface finishes walks through where each option fits, and the guide to PVD, Cerakote and anodizing covers the harder-wearing finishes.
4. Neutral salt spray is a screen, not a field life
A common mistake is to read a single NSS hour count as a promise of calendar-year service life. Neutral salt spray is a fast, repeatable comparison test. It is not the same as the cyclic corrosion that real vehicles and marine environments see, where salt, humidity, drying and temperature alternate.
For parts exposed on a vehicle or near the coast, many programmes now specify cyclic corrosion testing such as SAE J2334 alongside or instead of a plain NSS hour count. If your application is demanding, ask for the cyclic test up front. A part that passes 480 h of NSS but fails cyclic exposure is a part that will surprise you in service.
5. How to specify corrosion protection in an RFQ
Vague wording like “salt spray resistant” cannot be inspected. Write the requirement so it can be measured and accepted:
Hours and method (for example, 480 h neutral salt spray per ASTM B117 / ISO 9227 for Standard grade, or 720 h for Premium, or a named cyclic standard)
Acceptance (no white rust, or no red rust, or a minimum protection rating)
Sample scope (main faces only, or including edges and threads)
Coating build and pretreatment, since both drive the result
Stating these in the drawing and the quote avoids the worst kind of surprise: a finish that looks fine on paper and fails in week one. Our guide to reading a die casting quotation explains which lines on a quote cover finishing and inspection.
6. What we check before a part ships
For outdoor programmes we treat corrosion protection as a documented process, not a one-off test. That means controlled pretreatment, a specified coating system, and 480 h (Standard) / 720 h (Premium) salt spray verification on powder coated, electrocoated and plated parts as a standard check. Material certificates and first-article inspection back up the result so the evidence travels with the batch.
On top of the qualification, Sureton backs these systems with a 5-year warranty for Standard grade and a 10-year warranty for Premium grade on outdoor and UV service, because the result is controlled at the process level rather than left to chance. What we can do is name the test, the hours, the acceptance and the warranty, and show the data.
A 2026 note on finish chemistry for EU-bound parts
The corrosion screen and the chemical screen now travel together on any part heading into the EU. Alongside the 480 h or 720 h salt spray callout, RoHS and REACH shape which conversion coating and powder grade are allowed: chromate-free primers and TGIC-free powders are the versions finishing houses quote by default. None of this is a Sureton corrosion guarantee; it is the documentation the part needs so the coating that passes the test also clears the border. Put both the hours and the chemical system in the RFQ and the quote can name a route that satisfies each.
Need a salt spray specification that matches your environment?
Send the drawing, the service environment and the finish you have in mind. We will propose a coating system and the salt spray or cyclic corrosion check that proves it, with the acceptance written into the quote.
Related guides in this topic
Authoritative references
Independent third-party standards and industry bodies, provided for further reading. Sureton is not responsible for third-party content.


